Wuxi Weineng Automation Technology Co., Ltd. / Shandong Weineng Automation Technology Co., Ltd.
-
 [email protected]
-
 +86-18961722255


 English
 русский
 Español

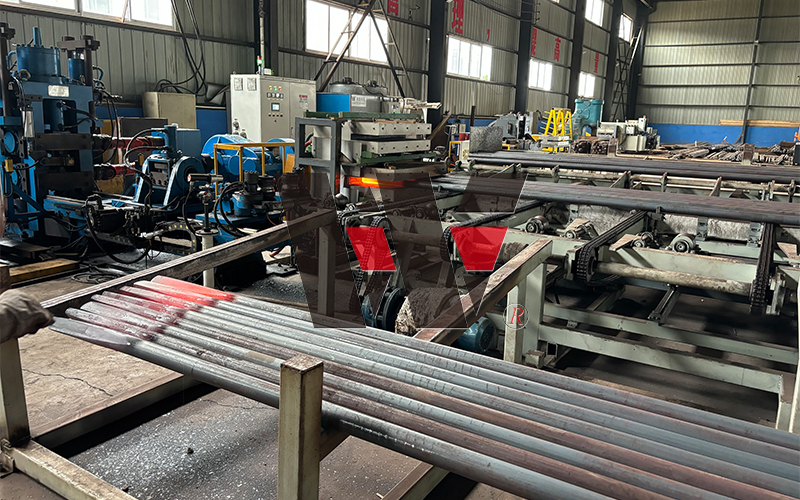
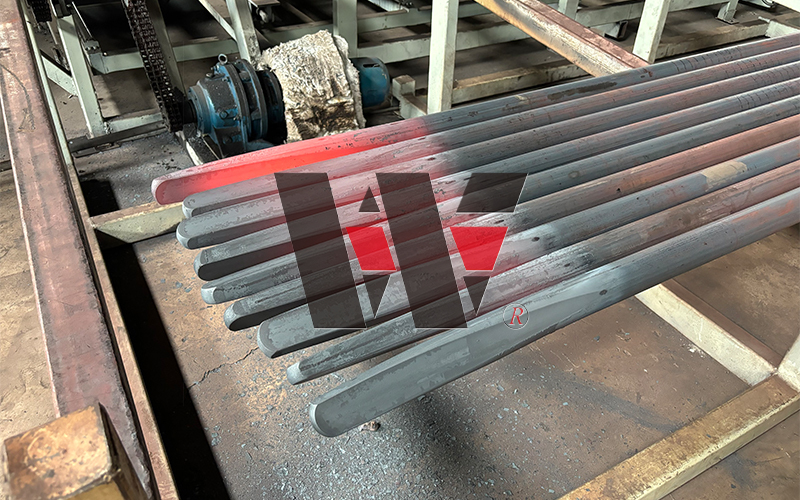
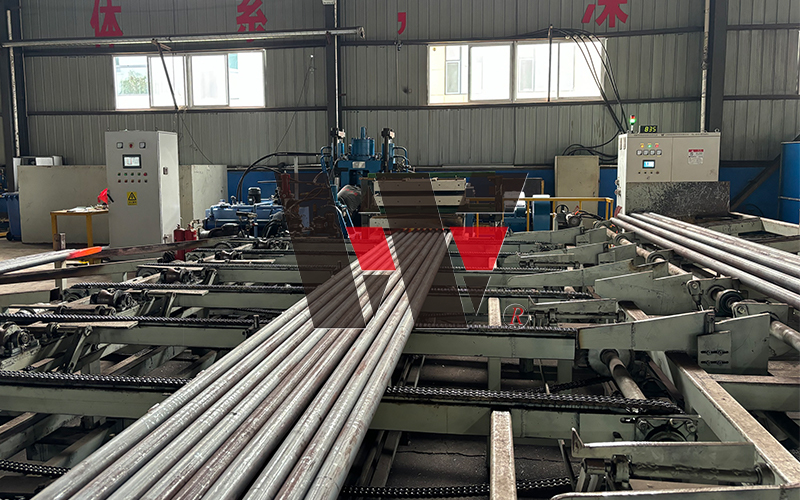
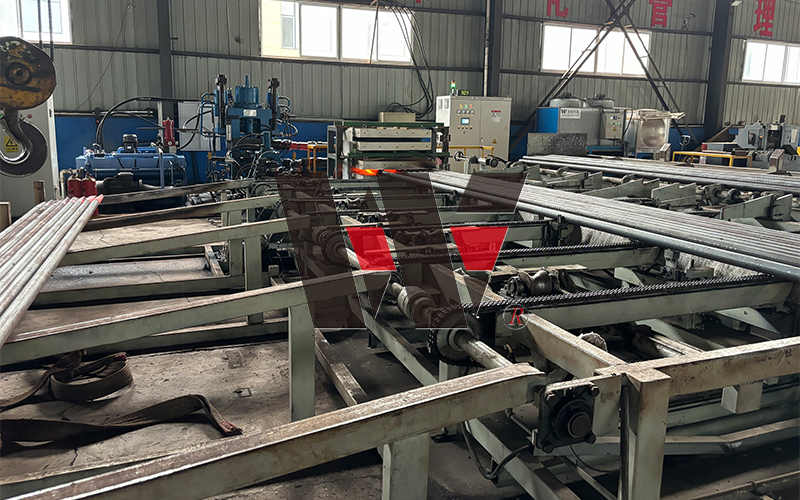
Hydraulic End Flattening Production Line
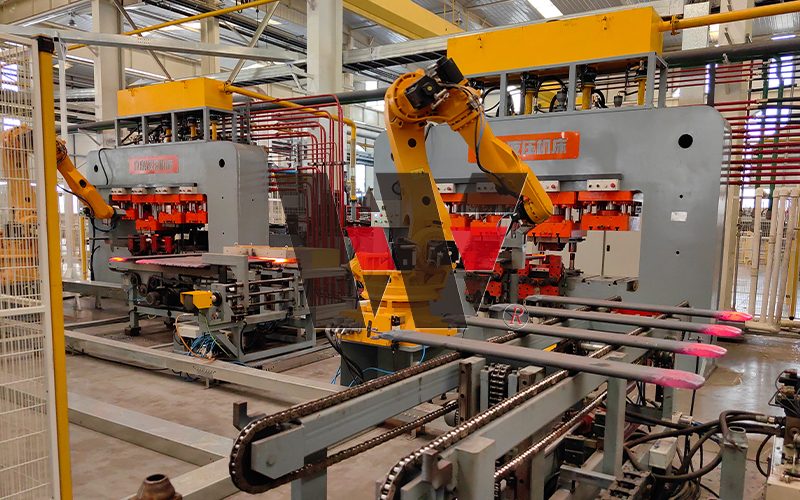
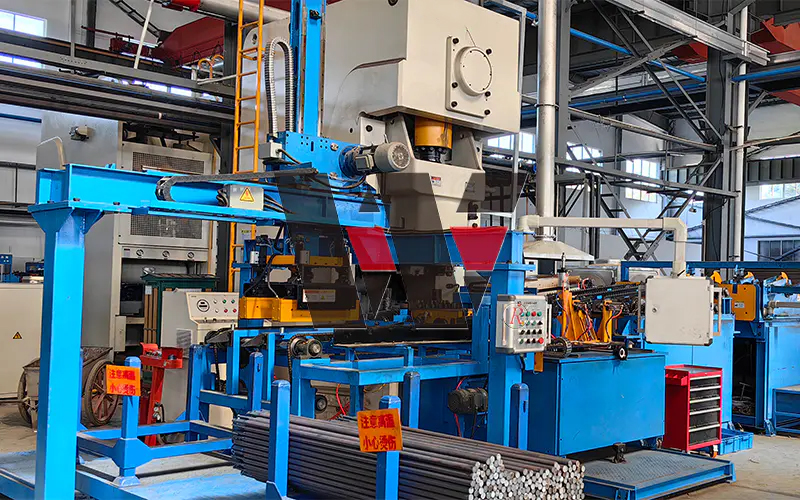
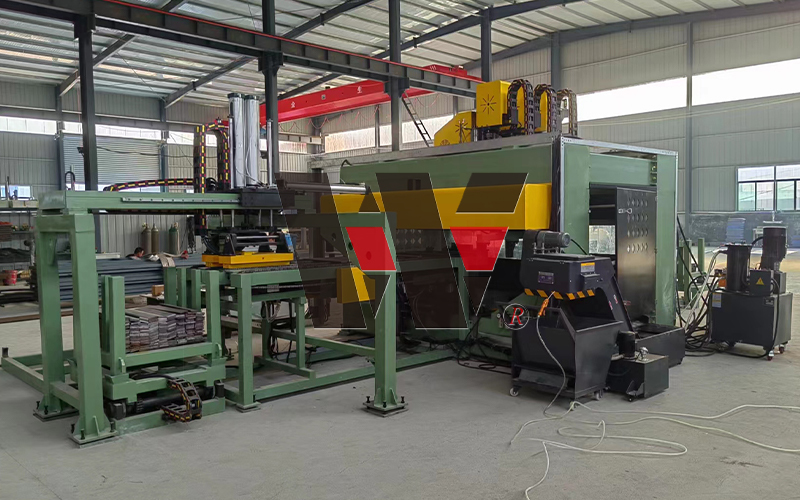
Hydraulic end flattening production line is engineered for precision end-forming of round bar or tubular workpieces such as springs and stabilizer bars, using a hydraulic drive system as the core actuating force. Working in conjunction with induction heating, it presses the round cross-section at each end into a flat profile to the tight geometric tolerances required by downstream eye-coiling, punching, and assembly operations.
The end-heating unit employs medium-frequency induction technology for fast, precisely targeted localized heating of the workpiece ends. Temperature is accurately set and controlled, ensuring the end material is fully softened to the optimal forming range while strictly confining the heat-affected zone to the end section, fully preserving the mechanical properties of the workpiece body.
The hydraulic drive delivers smooth, continuous, high-tonnage forming pressure. Compared to mechanical actuation, hydraulic output is more consistent and stroke position is more precisely controllable, enabling the line to handle larger cross-sections and higher-strength materials with ease. Pressure parameters can be readily adjusted to accommodate different workpiece specifications, supporting fast and flexible changeovers.
The close coordination between tooling and hydraulic cylinders ensures gradual and evenly distributed pressure application throughout the forming stroke, effectively eliminating the risk of end cracking or surface damage from impact forces. The resulting flat ends exhibit high dimensional consistency and excellent surface quality — well-suited to components with elevated precision and surface finish requirements.
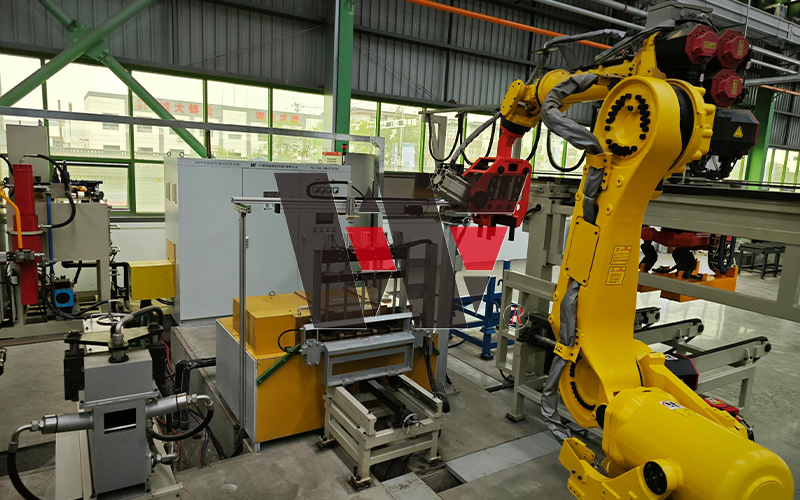
The line integrates induction heating, workpiece transfer, and hydraulic pressing in a fully automated and synchronized sequence with stable cycle times. The absence of open flames or high-voltage hazards makes for a safe and clean production environment. The compact, low-maintenance equipment configuration supports continuous, high-volume, multi-product production.
Related Products
About Us
Wuxi Weineng Automation Technology Co., Ltd.
Wuxi Weineng Automation Technology Co., Ltd. located in Wuxi, the Pearl of Taihu Lake, covers an area of 6,000 square meters and currently employs over 60 people. In 2016, the company's founding team began researching and developing complete sets of equipment for automotive leaf springs, hot-coiled springs, and stabilizer bars. Hydraulic End Flattening Production Line Supplier in China. To date, they have been deeply involved in this industry for 10 years and are recognized as a specialized, innovative, and distinctive enterprise in this field by the Ministry of Industry and Information Technology.
The company integrates R&D, production, sales, and service. Its main products include complete sets of automotive leaf spring equipment and stabilizer bar equipment, including stabilizer bar end induction heating equipment, stabilizer bar thermoforming induction heating equipment, hollow stabilizer bar double-end induction heating equipment, hollow bar resistance conduction heating production lines, stabilizer bar secondary vulcanization production lines, and hot-coiled spring equipment. The company also provides users with complete induction heating automated production lines. Hydraulic End Flattening Production Line Factory in China.
Over the years, the company has served leading domestic enterprises such as Shanghai China Spring Manufacturing Co., Ltd., Huawei Technology Co., Ltd., Zhejiang Meili Technology Co., Ltd., Zhejiang Jinsheng Auto Parts Co., Ltd., Chengdu ThyssenKrupp Fawer Spring Co., Ltd., Pinghu ThyssenKrupp (Pinghu) Automotive Stabilizer Bar Co., Ltd., and Liaoyang ThyssenKrupp Fawer Spring Co., Ltd., earning high praise for its products and services. Furthermore, the company has exported its equipment to countries such as Turkey, South Korea, India, Brazil, Egypt, Dubai, Iran, Africa, Tunisia and Morocco. "Professionalism, precision, innovation, and integrity" are the development concepts that the company has always adhered to. While continuously strengthening its own scientific research capabilities, it has formed stable industry-university-research cooperation with many universities. It has been repeatedly rated as a high-tech enterprise and a specialized and innovative enterprise. In the future, the company will continue to deepen its research and development in the automotive leaf spring, automotive guide arm, automotive stabilizer bar and spring industry equipment, provide the spring industry with more professional, intelligent and sophisticated equipment products, and contribute to the high-quality development of the global automotive leaf spring, automotive stabilizer bar and hot-coil spring industries.
News
-
Industry News Oct. 16. 2026
-
Industry News Oct. 10. 2026
-
Industry News Sep. 28. 2026
-
Do You Have Any Questions?
Let's
Discuss! -
Quick
Home Products / Equipment About Us Services Application News Contact Us -
Product Categories
Automobile Leaf Spring Complete Equipment Automobile Stabilizer Bar Complete Equipment Automobile Spring Complete Equipment Automotive guide arm complete equipment Oil Drilling Pipe Complete Equipment
-
Email Us
[email protected] [email protected] -
Address
Yangxiyuan Village, Luoshe Town, Huishan District, Wuxi City, Jiangsu Province, China -
Call Us Now
+86-18151713891 +86-18961722255 +86-18961507976 -
WhatsApp
+86-18151713891 +86-18961507976
Copyright © 2026 by Wuxi Weineng Automation Technology Co., Ltd. All Rights Reserved.
 Custom Hydraulic End Flattening Production Line Factory